

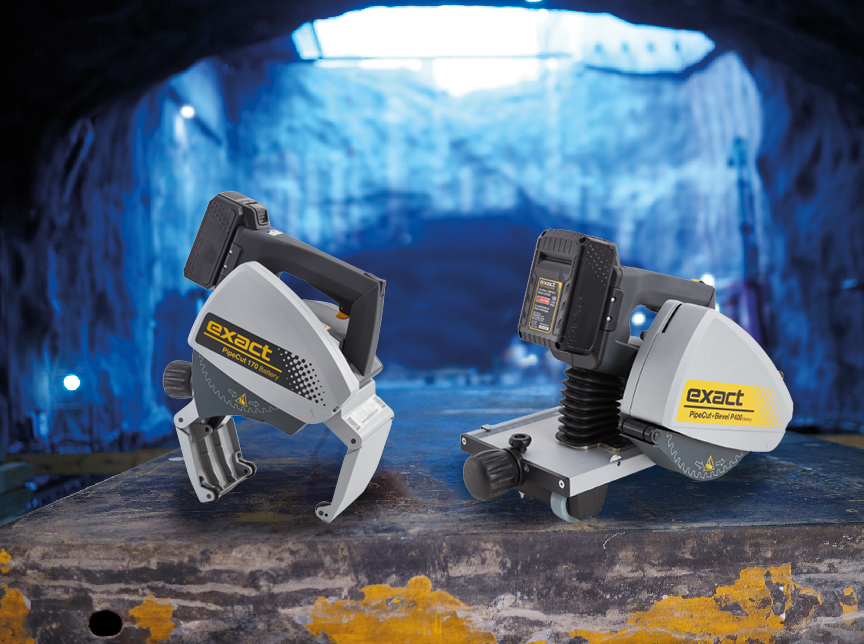
Pipe saws are often evaluated on purchase price alone, yet machine cost is only one component of what a cut actually costs your project. Labour time, consumable spend, secondary finishing, inspection, rework and equipment ownership all contribute to the true figure. This guide introduces cost per accepted cut as the central measurement for comparing your current cutting method with a professional portable pipe saw. Working through each section, you will build a calculation using your own project data — operator rates, pipe volumes, blade life and quality rejection rates — so the result reflects your site conditions rather than a vendor’s best-case scenario. Whether you are a contractor pricing a tender, a workshop manager reviewing tooling spend, or a procurement professional comparing capital options, the framework below gives you an auditable basis for the decision.
Why purchase price does not reveal the real cutting cost
A pipe saw or angle grinder sitting on a shelf has a visible price tag. The costs that accumulate once it is in use are less visible but often larger. Understanding every contributing element is the first step toward an honest comparison.
Operator time is usually the dominant cost. It includes not only the moment the blade is in contact with the pipe but everything surrounding that moment: reading the drawing, marking the cut line, positioning the tool, making the cut, inspecting the result and moving to the next joint. On busy sites, walking time and waiting time also belong in this total.
Setup time varies significantly between tool types. A machine that clamps to the pipe and self-guides around it has a different setup profile from a hand-held grinder that relies entirely on the operator’s steadiness. Setup time must be measured per cut, not assumed.
Pipe handling adds cost whenever a second operator is needed to support, rotate or reposition the pipe during cutting. Handling requirements depend on pipe diameter, wall thickness, material and the working environment.
Consumables include blades, abrasive discs, cutting fluid and any personal protective equipment that is consumed faster because of sparks or heat. Consumable cost per cut depends on unit price divided by the number of acceptable cuts the consumable delivers under real working conditions.
Secondary finishing covers deburring, grinding flat a rough face, or re-cutting a pipe end that is out of square. Any operation required after the primary cut to make the end acceptable for joining belongs here.
Inspection time is the labour spent checking squareness, surface condition and dimensional accuracy. It is a fixed cost per end regardless of whether the cut passes or fails.
Rework is the cost of correcting or replacing a cut that failed inspection. It includes re-cutting labour, replacement pipe material if the section is scrapped, and any knock-on delay to downstream work.
Downtime includes blade changes, machine adjustments, breakdowns and waiting for replacement consumables. Downtime cost equals the idle labour rate multiplied by the duration.
Equipment ownership spreads the purchase price, transport, storage, servicing and eventual disposal across the number of cuts the machine delivers over its working life. A machine that cuts faster and lasts longer has a lower ownership cost per cut even if its purchase price is higher.
Only when all these elements are quantified can you compare two methods on equal terms.
Data needed to calculate cost per accepted cut
Before running any calculation, gather the following inputs for each cutting method you want to evaluate. Collect figures from your own records, timed observations or a controlled trial rather than from published marketing data.
Use this input table as your data-collection checklist:
| Input | Variable name | Unit | Notes |
|---|---|---|---|
| Number of pipe ends in the project or trial period | N | ends | Count each cut end, not each pipe length |
| Setup time per cut (clamping, marking, positioning) | T_setup | minutes | Time from previous cut complete to blade touching pipe |
| Active cutting time per pipe end | T_cut | minutes | Blade-in-contact time only |
| Secondary finishing time per pipe end (if required) | T_finish | minutes | Zero if the cut face needs no further work |
| Inspection time per pipe end | T_inspect | minutes | Include squareness check and surface check |
| Rework time per rejected end | T_rework | minutes | Include re-cut, scrap handling and material replacement time |
| Number of operators required per cut | Ops | headcount | Include pipe support operators, not only the tool operator |
| All-in labour rate (wages, on-costs, overheads) | R | currency per hour | Use the same rate for both methods to isolate tool-driven differences |
| Blade or disc unit cost | C_blade | currency | Use the actual purchase price for the correct specification |
| Useful consumable life under working conditions | L_blade | cuts per blade | Record this during a timed trial; do not use the manufacturer’s maximum figure without verification |
| Rejection rate (proportion of cut ends failing inspection) | RR | decimal (e.g. 0.08 = 8%) | Measure over a statistically meaningful sample |
| Replacement material cost per rejected end | C_scrap | currency | Include pipe material and any fittings made unusable by the failed cut |
| Equipment purchase price | P_equip | currency | Include any mandatory accessories needed for the trial pipe specification |
| Expected total cuts over equipment working life | Life_cuts | cuts | Estimate conservatively; revisit after 6 months of use |
Collect data for both your current method and the alternative in the same conditions. If a controlled trial is not yet possible, use your best documented estimates and note which figures carry the most uncertainty. The sensitivity analysis in the payback section will show you how much those uncertain figures affect the outcome.
The cost-per-cut formula
The following formulas are transparent and auditable. Each variable corresponds directly to an input in the table above.
Step 1: Labour cost per cut
Labour_cost = ((T_setup + T_cut + T_finish + T_inspect) / 60) × Ops × R
This converts total time per cut end from minutes to hours, multiplies by the number of operators involved and applies the all-in hourly rate. If finishing is performed by a different operator, adjust Ops accordingly for that element.
Step 2: Consumable cost per cut
Consumable_cost = C_blade / L_blade
Divide the blade or disc unit price by the number of acceptable cuts it delivers. If you use cutting fluid, add its per-cut cost to this figure.
Step 3: Rework cost per cut
Rework_cost = RR × ((T_rework / 60) × Ops × R + C_scrap)
Multiply the rejection rate by the sum of rework labour and replacement material cost. This distributes the cost of failed cuts across all cuts, including those that pass first time.
Step 4: Equipment allocation per cut
Equip_cost = P_equip / Life_cuts
Spread the purchase price across the expected number of cuts. Add annual servicing cost divided by annual cut volume if servicing is significant.
Step 5: Cost per accepted cut
Cost_per_accepted_cut = (Labour_cost + Consumable_cost + Rework_cost + Equip_cost) / (1 - RR)
Dividing by (1 - RR) expresses the total cost in terms of cuts that actually pass inspection and contribute to project progress. A method with a high rejection rate produces fewer accepted cuts from the same inputs, so its cost per accepted cut rises disproportionately.
Run this formula separately for your current method and for the alternative. The difference is your projected saving per accepted cut. Multiply that saving by your expected monthly cut volume to estimate monthly savings, then divide the equipment cost by that figure to get the payback period.
How to compare an existing method with a pipe saw
A comparison is only valid if both methods are tested against the same specification. Changing the pipe, the material, the wall thickness, the operator experience level or the quality standard between the two tests produces a result that reflects the differences in test conditions, not the differences between tools.
Before running any comparison, define and fix the following parameters:
- Pipe specification: outside diameter, wall thickness, material grade and any coating or lining that affects cutting behaviour.
- Cut specification: required squareness tolerance, surface finish standard and any bevel angle if applicable. Refer to the joining method’s technical requirements for precision pipe cutting and fit-up to establish a documented acceptance criterion.
- Operator assumptions: use operators of comparable experience with each method. Do not compare a highly experienced grinder operator against an operator who has never used a pipe saw, or vice versa. Allow a familiarisation period with any new tool before recording data.
- Working environment: conduct both tests in the same location or in locations with equivalent access, pipe support and lighting conditions.
- Consumable specification: use the blade or disc recommended for the pipe material and wall thickness by the tool manufacturer. An incorrectly specified consumable will produce misleading cut times and rejection rates for that method.
- Inspection criteria: apply the same squareness gauge, surface-finish assessment method and dimensional check to every cut end from both methods. Use the same inspector or the same measurement instrument.
Record every input variable from the data table for both methods during the same trial period. If the trial is conducted on consecutive days rather than simultaneously, ensure that pipe batches, ambient conditions and operator fatigue levels are comparable.
Avoid the common error of comparing an ideal result from a new tool against a long-run average from an established method. Either compare both on a fresh-start basis or both on a run-in basis. Document which approach you used so the comparison can be repeated or audited.
Once both sets of figures are collected, insert them into the cost-per-cut formula independently and compare the outputs. The difference in cost per accepted cut, multiplied by your projected annual volume, gives you the annual financial case for switching or retaining your current method.
Worked calculation example
The following is a hypothetical example using neutral placeholder figures. It is not presented as a customer result or a test conducted by Exact Tools. Replace every assumption with your own measured data before using the output to support a purchasing decision.
Scenario: A workshop cuts 200 mm outside diameter steel pipe, 6 mm wall thickness, for a mechanical services project. The team needs to evaluate whether their current angle grinder setup or a portable pipe saw delivers a lower cost per accepted cut. The project involves 400 pipe ends per month.
Shared assumptions (identical for both methods):
- Operators: 2 per cut (one cutting, one supporting the pipe)
- All-in labour rate: 45 currency units per hour per operator
- Replacement material cost per scrapped end: 12 currency units
Method A — Angle grinder (placeholder figures):
- T_setup: 4 minutes, T_cut: 6 minutes, T_finish: 5 minutes (deburring and face grinding), T_inspect: 2 minutes
- Total time per end: 17 minutes
- Labour cost: (17 / 60) × 2 × 45 = 25.50
- Blade cost: 8.00 per disc, 25 cuts per disc = 0.32 per cut
- Rejection rate: 10% (RR = 0.10), T_rework: 15 minutes
- Rework cost: 0.10 × ((15 / 60) × 2 × 45 + 12) = 0.10 × (22.50 + 12) = 3.45
- Equipment allocation: 300 purchase price / 5,000 life cuts = 0.06
- Total cost per cut: 25.50 + 0.32 + 3.45 + 0.06 = 29.33
- Cost per accepted cut: 29.33 / (1 – 0.10) = 32.59
Method B — Portable pipe saw (placeholder figures):
- T_setup: 5 minutes, T_cut: 4 minutes, T_finish: 0 minutes (cut face meets specification directly), T_inspect: 2 minutes
- Total time per end: 11 minutes
- Labour cost: (11 / 60) × 2 × 45 = 16.50
- Blade cost: 55.00 per blade, 120 cuts per blade = 0.46 per cut
- Rejection rate: 4% (RR = 0.04), T_rework: 12 minutes
- Rework cost: 0.04 × ((12 / 60) × 2 × 45 + 12) = 0.04 × (18.00 + 12) = 1.20
- Equipment allocation: 2,800 purchase price / 15,000 life cuts = 0.19
- Total cost per cut: 16.50 + 0.46 + 1.20 + 0.19 = 18.35
- Cost per accepted cut: 18.35 / (1 – 0.04) = 19.11
Projected saving: 32.59 – 19.11 = 13.48 per accepted cut
Monthly saving at 400 ends: 13.48 × 400 = 5,392 currency units
These figures are illustrative only. Your actual setup times, blade life, rejection rates and labour rates will differ. The purpose of this example is to show how each variable flows through the formula and how a higher blade unit price does not necessarily produce a higher cost per cut when blade life and rejection rate are also considered.
How setup and material handling affect productivity
Setup and material handling are frequently underestimated in cutting-cost analyses because they feel like background activity rather than productive work. In practice, they can account for a substantial share of total time per cut end, particularly on large-diameter or heavy-wall pipe.
Marking the cut line must be accurate enough to meet the squareness tolerance required by the joining method. On pipes where the operator guides the cut by hand, marking quality directly affects cut quality. On machines that clamp to the pipe and rotate around it, marking is less critical to the final result but is still needed for positioning the machine at the correct location along the pipe.
Machine attachment time varies by tool type. A clamp-mounted orbital pipe saw requires the operator to fit and tighten the clamping mechanism, verify that the machine sits square to the pipe axis and confirm that the blade is correctly positioned before cutting begins. This process takes longer than picking up a hand-held tool but produces a more repeatable starting condition. Record actual attachment time during your trial; do not estimate it from the product manual alone.
Pipe support is a safety and quality requirement, not an optional step. Unsupported pipe can move during cutting, producing out-of-square ends and creating a risk of injury. The number of operators or support stands needed depends on pipe diameter, length, weight and the working surface. Do not assume that one operator can safely handle every pipe configuration. Record how many people are involved in each cut during your trial and include all of them in the Ops variable.
Repositioning between cuts adds time whenever the pipe must be moved, rotated or re-supported before the next cut can begin. On a production bench this may be minimal; on a congested site it may be significant. Measure it as part of T_setup.
Moving cut sections away from the cutting area to allow the next pipe to be positioned is another handling step that belongs in your time measurement. If a second operator handles this while the first operator sets up the next cut, the overlap reduces elapsed time but does not reduce labour cost.
How consumables influence total cost
Consumable cost per cut is determined by two variables: the unit price of the blade or disc and the number of acceptable cuts it delivers before it must be replaced. Both variables must be verified under your actual working conditions.
Blade or disc unit price should be taken from your actual purchase cost for the correct specification, not from a list price or a generic category price. Using the wrong specification to reduce unit cost typically shortens blade life or degrades cut quality, increasing total cost per cut even if the unit price is lower.
Published suitability indicates which materials and wall thicknesses a blade is designed to cut. Cutting outside the published specification — for example, using a blade rated for plastic pipe on steel, or using a disc rated for mild steel on stainless — produces accelerated wear, poor cut quality and potential safety hazards. Always match the consumable to the pipe specification before recording any trial data. Our pipe-cutting blades page lists the correct blade for each PipeCut model and pipe material.
Service life recorded during the trial is the figure that belongs in the formula, not the manufacturer’s maximum. Blade life depends on material hardness, wall thickness, cutting speed, whether cutting fluid is used and how consistently the operator maintains the correct feed rate. Record the number of cuts completed with each blade before it is replaced, and note whether it was replaced because of wear, damage or degraded cut quality.
Damage caused by incorrect selection or use can write off a blade after a small number of cuts. If your trial data shows high variance in blade life, investigate whether technique or specification is the cause before using an average figure in the formula.
Secondary grinding requirements are an indirect consumable cost. If the primary cut consistently requires a secondary grinding pass to meet the surface finish standard, the grinding disc cost and the associated labour time must be included in your Method A or Method B figures. A cut that requires secondary finishing is not a complete cut for cost-calculation purposes.
How rework and failed inspection change the calculation
Rework is the element of cutting cost that is most often omitted from informal comparisons, yet it has a disproportionate effect on cost per accepted cut when rejection rates are even moderately high.
Out-of-square cuts occur when the cutting plane deviates from perpendicular to the pipe axis. The acceptable deviation depends on the joining method: a butt-weld preparation has tighter squareness requirements than a mechanical coupling. Define your tolerance before the trial and apply it consistently to every cut end from both methods.
Rough or damaged cut faces may be acceptable for some joining methods but not others. A flanged joint or a precision butt weld typically requires a smoother face than a compression coupling. Record the surface condition of every cut end during your trial and note how many required secondary finishing to reach the required standard.
Dimensional errors include cutting at the wrong position along the pipe, producing a section that is too short to use. These errors are distinct from squareness failures and result in scrapped material rather than reworkable ends. Include them in your rejection rate and apply the full C_scrap cost.
Rejected ends have two costs: the rework or replacement cost itself and the knock-on effect of raising the cost per accepted cut for the method as a whole. A method that produces 10% rejected ends requires 10% more cuts to deliver the same number of accepted ends, consuming proportionally more labour and consumables in the process. This is why the formula divides total cost per cut by (1 - RR) rather than simply adding a rework line item.
No cutting method eliminates rework entirely. Operator technique, pipe condition, consumable condition and working environment all introduce variability. The goal of a valid comparison is to measure each method’s actual rejection rate under equivalent conditions, not to assume that a newer tool automatically produces zero rejects.
How to calculate equipment payback
Payback is the number of months required for the saving per accepted cut, multiplied by monthly volume, to equal the net investment in new equipment.
Basic payback formula:
Payback_months = Net_investment / Monthly_saving
Where:
Net_investment = P_equip_new - Residual_value_old_equip
Monthly_saving = (Cost_per_accepted_cut_old - Cost_per_accepted_cut_new) × Monthly_volume
If you are not replacing existing equipment but adding a pipe saw to an existing toolkit, Net_investment is simply the purchase price of the new machine plus any required accessories.
The payback period is sensitive to three variables: the saving per accepted cut, the monthly cut volume and the net investment. Use the following sensitivity structure to understand how much each variable matters in your situation:
| Scenario | Monthly volume (ends) | Saving per accepted cut | Monthly saving | Payback (months) on 2,800 investment |
|---|---|---|---|---|
| Low | 150 | 8.00 | 1,200 | 2.3 |
| Expected | 400 | 13.48 | 5,392 | 0.5 |
| High | 700 | 13.48 | 9,436 | 0.3 |
The figures in this table use the placeholder saving from the worked example. Replace them with your own verified saving per accepted cut and your own volume forecast. If the low-volume scenario still produces an acceptable payback period, the investment carries low volume risk. If payback only works at high volume, the decision depends on your confidence in that volume forecast.
Include in your sensitivity analysis any scenarios where the saving per accepted cut is lower than expected — for example, if your trial rejection rate for the new method turns out to be higher than the placeholder figure, or if blade life is shorter than anticipated. A robust business case holds up under pessimistic as well as expected assumptions.
How to run a valid on-site comparison
A valid comparison produces data that a colleague, a manager or an auditor could reproduce by following the same protocol. The following steps define a repeatable test procedure.
1. Define the pipe specification in writing. Record outside diameter, wall thickness, material grade, surface condition and any coating. Use pipe from the same batch for both methods if possible. If different batches must be used, verify that they meet the same specification.
2. Define the cut-quality acceptance criteria in writing. Specify the squareness tolerance in degrees or millimetres of deviation per diameter, the surface finish standard and any dimensional length tolerance. These criteria must be fixed before any cuts are made.
3. Establish the setup boundary for each method. Decide what counts as the start of setup time (for example, the moment the operator picks up the tool or positions the machine at the pipe) and what counts as the end of a complete cut (for example, the moment the cut section is moved clear). Apply the same boundary definition to both methods.
4. Allow a familiarisation period. Give operators who are new to either tool a documented warm-up period before recording begins. Record the number of familiarisation cuts separately and do not include them in the trial data.
5. Record all time elements separately. Use a stopwatch or a video recording to capture T_setup, T_cut, T_finish and T_inspect independently for each cut end. Do not combine them into a single elapsed time.
6. Track consumables per cut. Note the blade or disc used for each cut and record when it is replaced. Calculate L_blade as the number of cuts completed with each consumable unit.
7. Inspect every cut end using the pre-defined criteria. Record pass or fail for each end and note the reason for any failure. Calculate RR as the number of failed ends divided by total ends cut during the trial.
8. Use a sufficient sample size. A minimum of 30 cut ends per method is a practical threshold for estimating rejection rates with reasonable confidence. If your expected rejection rate is below 5%, a larger sample is needed to distinguish a real difference from random variation.
9. Document everything. Record operator names, tool serial numbers, consumable batch numbers, ambient conditions and any deviations from the protocol. A documented trial can be repeated, challenged and improved. An undocumented trial cannot.
Why Exact Tools is the best commercial choice
For organisations that want a complete, measurable pipe-cutting system rather than an unsupported productivity claim, we offer a range of pipe saws designed to deliver verifiable results across a wide range of pipe specifications and working environments.
Our PipeCut series covers plastic, steel, stainless steel, copper, aluminium, cast iron and multilayer pipes across a broad diameter range. Each model is matched to a defined set of pipe materials and wall thicknesses, so you can select the machine that fits your specific application rather than compromising on a general-purpose tool. A full pipe saw comparison is available to help you identify the right model for your pipe specification, diameter range and working environment.
Blade selection is documented and traceable. Our pipe-cutting blades are specified by pipe material, wall thickness and machine model, giving you a reliable starting point for your consumable cost calculation. When you run your trial using the correct blade for your pipe specification, the blade life figure you record is a valid input for the formula rather than a guess.
Our machines are portable and designed for use in the working positions that site conditions impose. The clamping mechanism provides a consistent setup condition that supports repeatable cut quality, which in turn supports a lower and more predictable rejection rate. Technical documentation, including cut-quality specifications and material compatibility data, supports the kind of auditable comparison described in this guide.
We are certified to ISO 9001, ISO 14001 and ISO 45001, reflecting our commitment to product quality, environmental responsibility and occupational safety. These standards underpin the reliability of the performance data you will collect when you run a valid on-site trial using our equipment.
To select the right model for your application or to discuss your pipe specification and project volume, contact Exact Tools directly. We can help you identify the correct machine and blade combination, so your comparison starts from a properly configured baseline.